

TKE 554
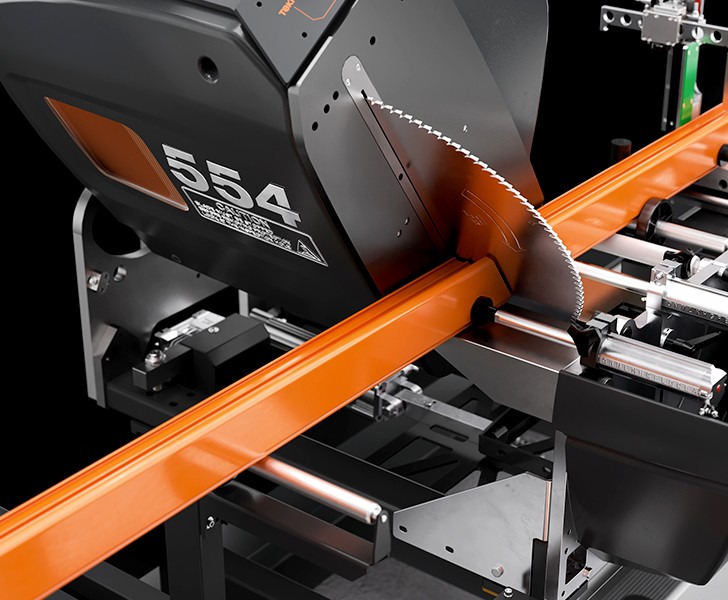
Twin-head cutting-off machine with 3 controlled axes with automatic movement of the mobile head and electronic control of every angular setting within the range 45° (internal) to 22°30' (external). The feeding of the two 550 mm blades is driven by hydro-pneumatic cylinders.
Technical data

Included
Available
Profile clamping
The profile to be cut is clamped by two horizontal hold-down devices with extreme precision and in absolute safety. For vertical clamping, particularly for special cuts, the machine can be equipped with a patented system of horizontal hold-down devices. When two considerable lengths are cut, the profile is supported by a manually positioned intermediate support.
Head guards
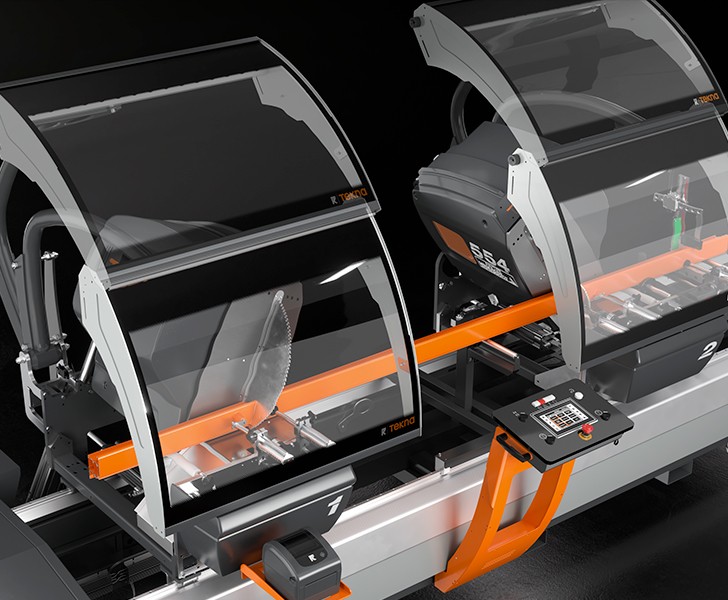
The machining zone is protected by two automatically positioned local guards installed on the cutting units. The guards are made of scratch-proof polycarbonate and they are opened/closed automatically by a pneumatic cylinder at the appropriate points of the cutting cycle.
Load and unload
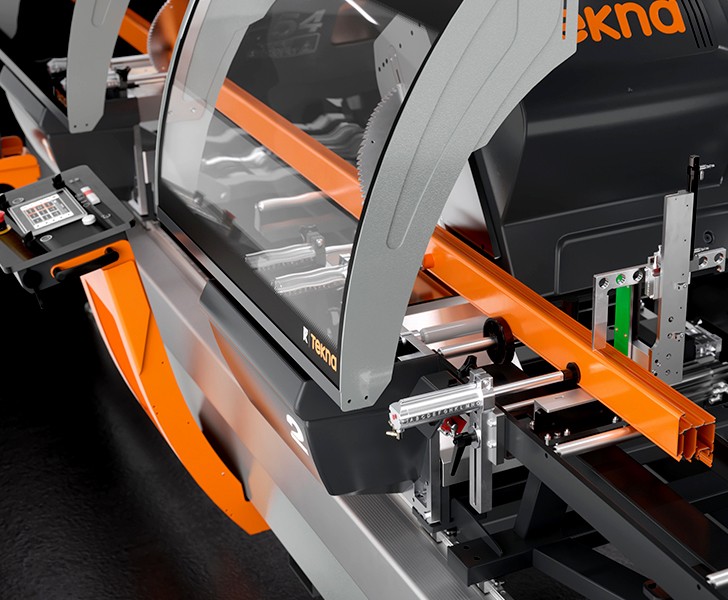
The cutting-off machine is equipped with a roller conveyor on a mobile head for standard loading and unloading procedures. The roller conveyor can be optionally fitted with an extra vice to immobilise the residual profile and an electronic machined profile thickness meter for automatic cutting positions correction in accordance with the real profile dimensions, with the associated surface treatments tolerance.

Control
The control panel, installed on a support sliding on bearings along the front side of the machine, allows correct mobile heads positioning in accordance with the required cutting schedule. The interface uses a 7” touch-screen and fully personalised software and is packed with bespoke functions that are unique to this machine. The machining cycle can be optimised by creating cutting lists, thereby reducing scrap and cycle times for parts loading-unloading.
Heads tilting
Servomotors with encoders provide the tilting of the mobile units, and the relevant positioning is electronically managed and parameterised by the control, which features a simple and intuitive operator interface.
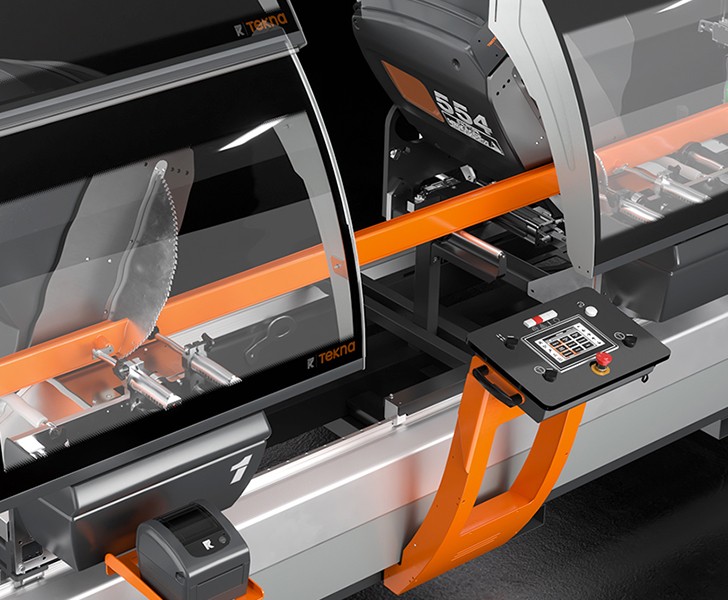
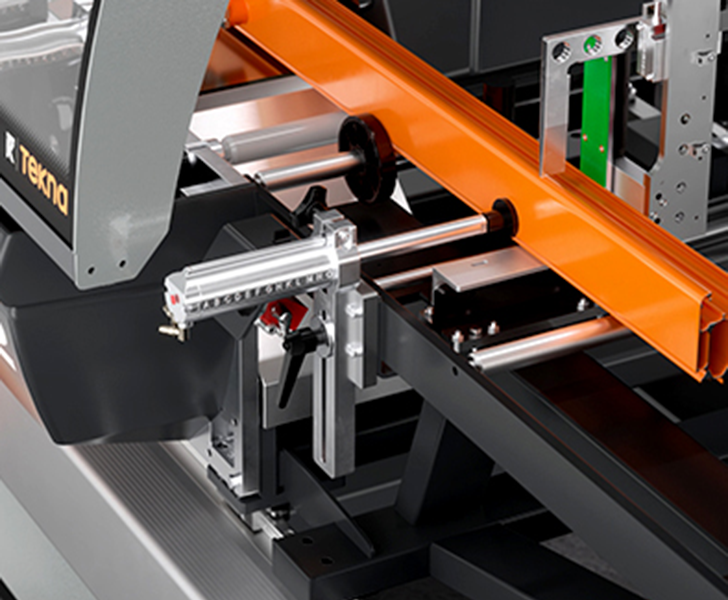
Additional vice for profile support on mobile head roller conveyor (Optional)
After each cut, the remaining profile short cut tends to fall on the roller conveyor, with the risk of hitting against the blade when the cut-off phase is still in progress. This movement may damage both the workpiece itself and the one just cut. The additional vice installed on the roller conveyor prevents this problem by keeping the profile locked for the entire duration of the cut-off cycle.